F=ΔpA can screen ideal static holding force for SMT nut pickup. Δp is the pressure difference between ambient air and the pickup region; A is the actual effective suction area. Nozzle outside diameter and maximum vacuum-source rating are not substitutes for these inputs. Static pickup does not validate acceleration, rotation or stopping.
Define pressure and area
Schmalz's suction-cup design explanation states the pressure-area relation as purely static and without a safety factor. Applying that principle to an SMT nut is a screening calculation; nozzle geometry and machine parameters still need equipment-supplier approval.
For hypothetical differential pressure 50 kPa=50000 Pa and an established effective sealed area of 4 mm²=4×10⁻⁶ m², F=0.20 N. The area is an assumed input, not a conversion from a nozzle diameter. A −50 kPa vacuum reading requires confirmation of its gauge-pressure reference; it is not negative absolute pressure.
Draw the sealing boundary around the threaded opening
A central bore, chamfer, step or offset contact may prevent sealing. Mark contact surfaces and air paths on an actual photograph or section and check whether the nozzle spans the through-hole. Without an established seal, neither full outside-diameter area nor an arbitrary annular area is a validated effective pickup area.
| Item | Record | Invalid shortcut |
|---|---|---|
| Differential pressure | Loaded pickup value and sensor position | Unloaded source limit |
| Effective area | Equipment-approved sealing boundary | Nozzle diameter or entire nut top |
| Timing | Evacuation, lift permission and release | Static final reading alone |
| Motion | Speed, acceleration, rotation and stopping | Slow manual pickup alone |
Check leakage before raising a setpoint
Festo's vacuum-technology guidance explains that leakage affects attainable vacuum and can originate at tubing, fittings or the workpiece interface. Use approved machine diagnostics to compare the pickup pressure trace and distinguish interface, air-path and height issues.
Review filters, connections and vacuum-confirmation logic without bypassing alarms. A changed nozzle, pickup aid or surface requires checks for thread, coating, cleanliness and reflow compatibility. Temporarily blocking a functional hole is not a validated production change.
Validate the real handling cycle
Use the actual feeder, nozzle, orientation and motion program. Record pickup failures, in-motion drops and placement errors separately, then compare one controlled variable using the equipment supplier's procedure. Keep guards and interlocks active and hands outside operating machinery.
For an SMT nut inquiry, provide mass, pickup region, bore geometry, packaging direction and machine information. For a different process stage, see post-reflow nut floating and tilt.
Questions
Is force greater than weight sufficient? Review dynamic loads, eccentricity, contact state and equipment-required margins as well.
Is a larger nozzle always better? It must fit a sealable region; spanning an opening can increase leakage.
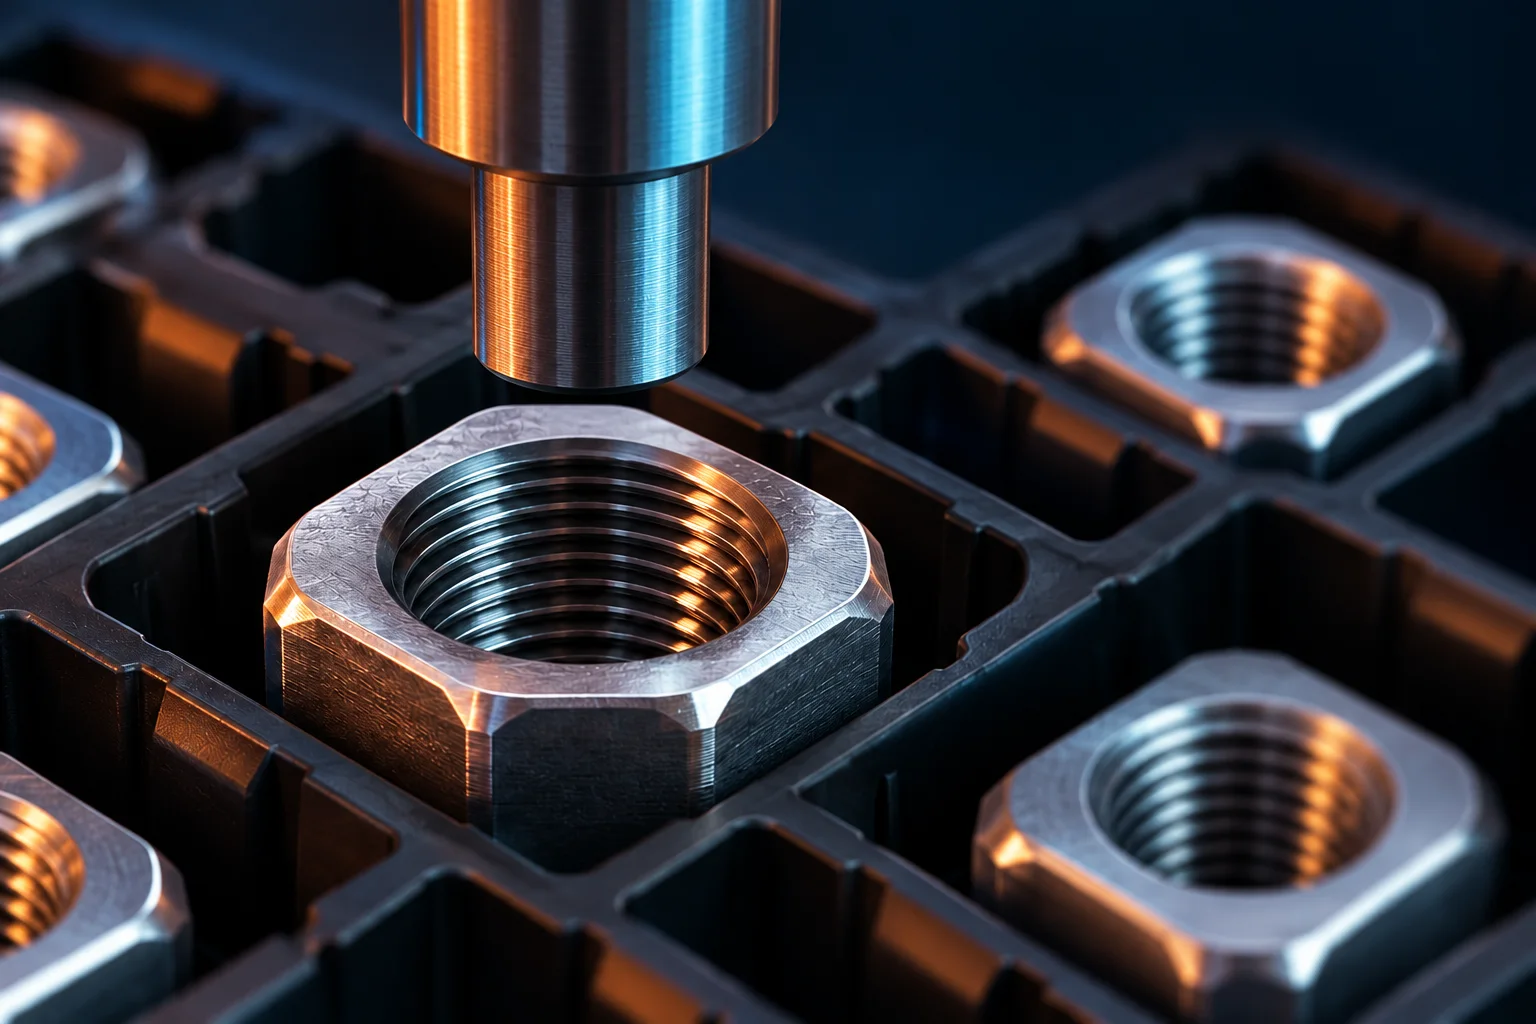
The AI-generated cover plans a pickup region; it does not show a validated nozzle or measured force. The example is not a Hongchuan placement-capability or machine-setting claim.